1. Start with representative feed-water data
Provide a recent analysis including conductivity or TDS, hardness, alkalinity, pH, chloride, sulfate, silica, iron, manganese, turbidity and temperature. Depending on the source, SDI, organics, microbiology, free chlorine and seasonal variation may also be required.
Identify whether the source is municipal, well, surface water, brackish water, seawater or treated wastewater. A single sample that does not represent seasonal or operational variation can produce an unreliable design.
2. Define product water and operating targets
State the required net product flow, operating hours, product-water quality, recovery target, redundancy philosophy and expected availability. Clarify whether flow is required at the design temperature or at the coldest operating condition.
The design should show expected feed, permeate and concentrate flows, membrane flux, salt rejection assumptions and the conditions used for projection.
3. Treat pretreatment as part of the RO system
Pretreatment may include oxidation or dechlorination, clarification, multimedia filtration, activated carbon, softening, antiscalant dosing, ultrafiltration and cartridge filtration. The correct route depends on the feed source and membrane risk.
Dosing chemicals, cartridge rating, monitoring points, clean-in-place philosophy and waste streams should be visible in the scope rather than left as assumptions.
4. Specify components and maintainability
Request declared brands and models for pumps, membranes, pressure vessels, instruments, valves and control hardware. Check material compatibility, duty point, motor efficiency, local voltage and the availability of service support in the destination market.
Layouts must allow membrane removal, pump and cartridge maintenance, sampling and safe chemical handling. The lowest footprint is not necessarily the best operating layout.
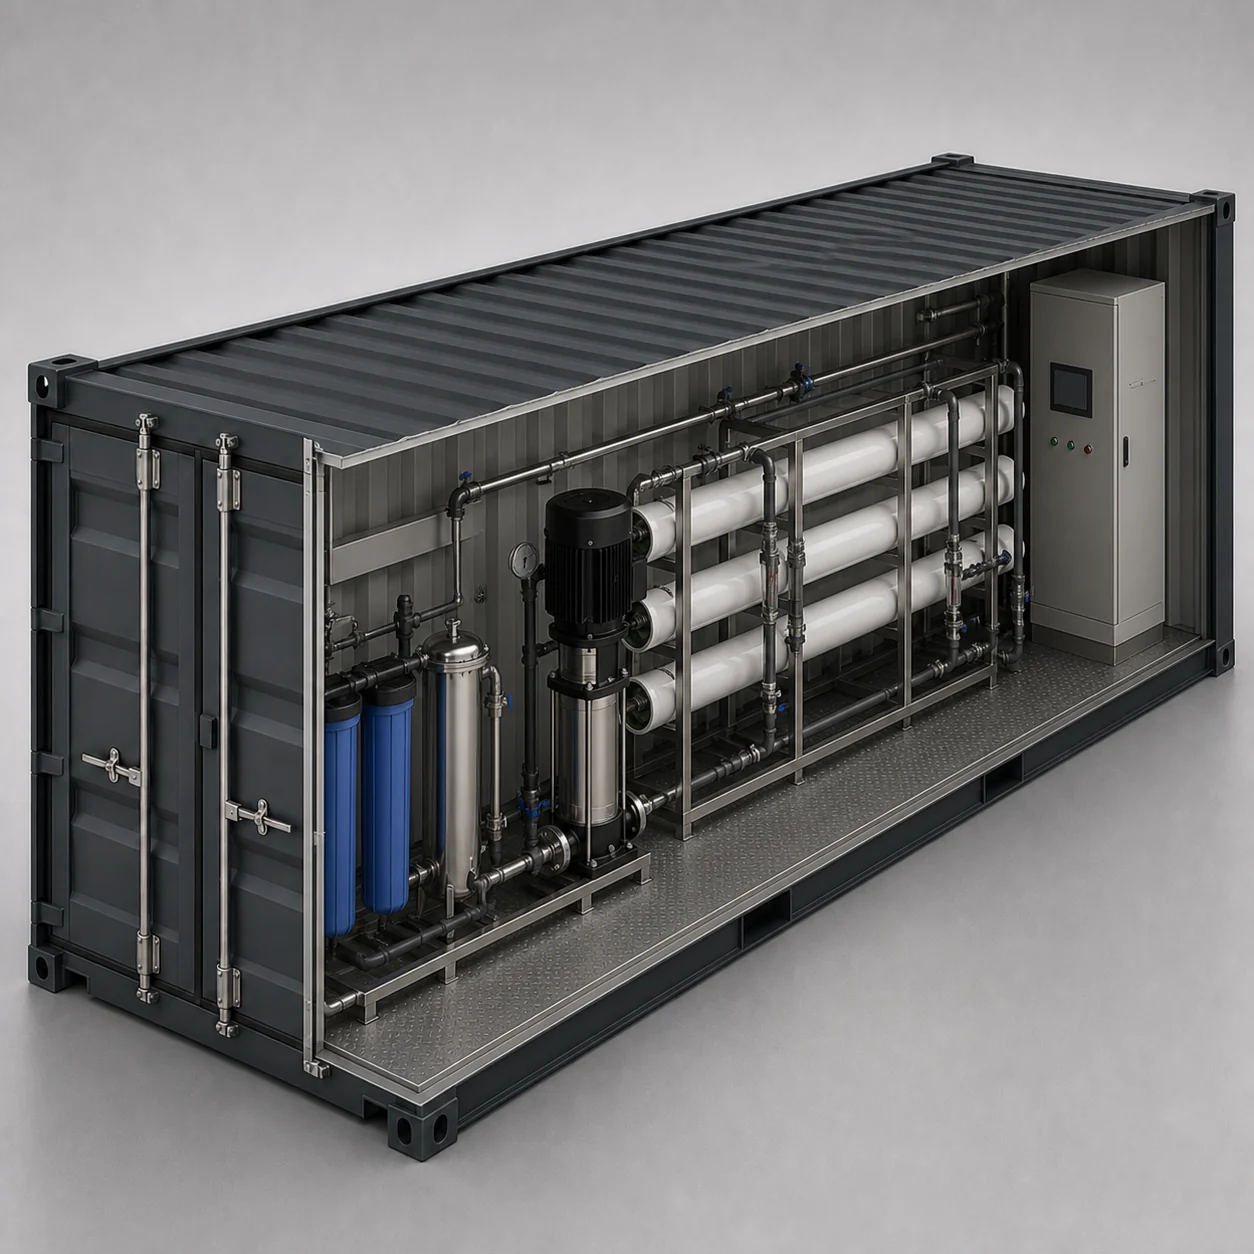
5. Decide whether containerization adds value
A container can simplify transport and site work, but it must be engineered as an equipment room. Confirm climate, insulation, ventilation, drainage, lighting, chemical segregation, emergency access, lifting and maintenance clearances.
Use practical personnel access—normally a correctly sized door at an accessible end or location—and avoid unnecessary openings that weaken weather protection or reveal an unbuildable arrangement. A cutaway render should be treated as an explanation of layout, not as the construction drawing.